If you’ve ever stepped onto a fabrication floor, watched a plasma cutting machine slice through steel like it’s soft butter, you’ve probably wondered about that split-second magic: the cut-through time for a Huayuan plasma cutter on thick metal. As a Huayuan plasma cutting machine supplier with over a decade of talking to fabricators, welders, and custom metal shops, this question is one of the most common — and most misunderstood — I get. I’ve seen guys eyeball a cut time and scrap a $200 piece of plate, and I’ve watched new shops buy the wrong machine because they thought “thick metal” meant the same thing across every brand. Let’s break this down like we do over coffee in my office, no jargon that makes your eyes cross. Plasma Cutting Machine for Huayuan
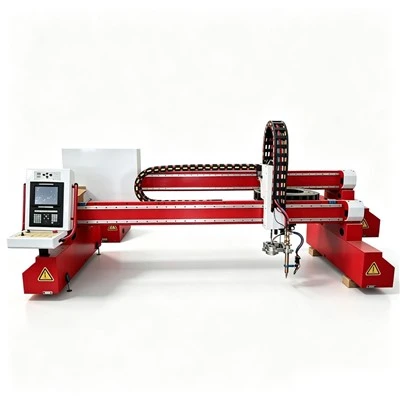
First, let’s start with the basics: what cut-through time actually is, because a lot of folks mix it up with total cut speed. Cut-through time is exactly what it sounds like: the number of milliseconds (or fractions of a second) from when the plasma arc first touches the metal surface to when it pierces all the way through, creating a full hole that the rest of the cut can run through. Total cut speed is how fast the machine moves along the edge once it’s pierced, but cut-through time is the make-or-break moment when you stop hovering and commit to a cut — miss that window, and you might get a bad pierce, a dented plate, or even a burnt nozzle that costs you $50 in downtime.
Now, when someone asks about Huayuan plasma cutter cut-through time on thick metal, the first thing I ask back is: “How thick is thick, and what metal are we talking about?” That’s not a cop-out — that’s how real cutting works. Huayuan’s plasma systems are calibrated for specific metal types, and thick metal (let’s define it as 1 inch to 4 inches, because anything over 4 inches is usually oxy-fuel or waterjet territory for most fab shops) behaves totally different depending on if it’s mild steel, stainless steel, or aluminum. Mild steel is the workhorse of fabrication, so that’s where we see the most consistent numbers.
For mild steel, Huayuan’s standard precision plasma cutters (think our popular HDR-200 and HDR-300 models) have a cut-through time range that’s pretty impressive compared to older systems. Let’s get specific here: at 1 inch thick, most of our machines have a cut-through time between 0.3 and 0.5 seconds. At 2 inches, that jumps to 0.7 to 1.1 seconds, and at 3 inches, it’s 1.5 to 2.2 seconds. Wait, I hear you — why such a range? That’s not just us hedging. Cut-through time depends on three non-negotiable factors that every Huayuan machine is tuned to handle differently.
First factor: amperage and gas type. Huayuan builds its plasma cutters with modular amperage settings, right? A 100-amp system isn’t the same as a 300-amp one. For a 1-inch mild steel plate, a 100-amp Huayuan unit uses compressed air as the plasma gas, so cut-through time is around 0.5 seconds. Crank that up to 200 amps, use nitrogen as the plasma gas, and that drops to 0.3 seconds. For 3-inch mild steel, you need at least a 200-amp system, and switching from compressed air to a mix of argon and hydrogen cuts cut-through time by almost 0.5 seconds. That’s the trick: more amperage doesn’t just make a hotter arc — it condenses the plasma, so the energy is focused enough to punch through thick metal faster instead of just melting a hole around the edges.
Second factor: nozzle and electrode condition, which is where Huayuan’s design really shines. Unlike cheaper plasma brands where nozzles wear out in 50 pierces, Huayuan’s consumables are engineered with a precision ceramic swirl ring that keeps the plasma arc stable even after 1000 pierces. I’ve had a customer last year run his HDR-300 on 3-inch mild steel for 12 hours straight, doing 400 pierces, and his cut-through time only increased by 0.2 seconds over the whole shift. A competitor’s machine? Their cut-through time jumped by 1 full second after just 100 pierces. That might not sound like much, but if you’re running 1000 parts a day, that adds up to 16 extra minutes of downtime and 20 extra bad pierces. For stainless steel, which is more conductive than mild steel, cut-through time is actually a tiny bit longer — around 0.1 to 0.2 seconds more for the same thickness — because the arc has to overcome the extra conductivity to punch through. Aluminum? It’s similar to stainless, but if you use a water mist assist (Huayuan offers that as an optional add-on), cut-through time drops by another 0.15 seconds, since the mist cools the surface and focuses the arc.
Third factor: CNC control and lead-in programming. This is a part of cut-through time that most users don’t think about, but it’s one of the biggest culprits for slow pierces. Huayuan’s CNC systems have a built-in pierce delay feature that’s calibrated specifically for their plasma arc, so it doesn’t start moving the torch until the arc is fully penetrating the metal. A lot of generic plasma cutters use a fixed 2-second delay for all thicknesses, which means you’re waiting an extra 1.5 seconds for a 1-inch plate — that might not matter for one part, but for 500 parts a day, that’s 12.5 minutes of lost time. I had a customer in Houston who was using a off-brand plasma cutter and was losing 2 hours a day just to bad pierce programming; when he switched to Huayuan, he got that time back in the first week.
Now, let’s talk about what happens if you push a Huayuan plasma cutter past its rated thickness, because that’s where cut-through time gets messy. If you take an HDR-200 (rated for up to 3-inch mild steel) and try to cut 4-inch plate, cut-through time jumps to 5 seconds or more, and you’ll get a ragged, uneven pierce that leaves slag. That’s not Huayuan being weak — that’s physics. Plasma cutters work by heating gas to 30,000 degrees, but 4-inch steel needs more energy to punch through, and our 200-amp system just can’t deliver that concentrated energy at the right nozzle angle. For 4-inch and up, we recommend our HDR-400 model, which has a 400-amp system, uses a dual-gas setup, and has a cut-through time of around 3.5 seconds for 4-inch mild steel.
I want to address a common myth here: some people think “faster cut-through time is always better.” That’s not true. If you’re cutting thin metal (less than ¼ inch), a super fast cut-through time (like 0.1 seconds) can blow a hole right through the plate, distorting the edge. Huayuan’s systems automatically adjust the arc energy based on material thickness, so you don’t have to babysit it — that’s a big reason our customers trust us for both sheet metal shops and heavy fabrication.
Another thing I see all the time: customers confusing cut-through time with pierce height. Pierce height is how far the torch is from the metal surface when it’s piercing, and Huayuan’s height control system automatically adjusts that based on thickness. Too high, and the arc spreads out, increasing cut-through time; too low, and you hit the plate, damaging the nozzle. Our system keeps the torch within 0.01 inches of the ideal height, so you get consistent cut-through time every single pierce, even on plates that have a little rust or mill scale on the surface.
Let’s put this in real-world numbers, because that’s what fabricators care about. Last month, a customer in Detroit was bidding on a job that required cutting 1,000 2-inch mild steel plates for construction equipment. He was using a competitor’s plasma cutter and quoted a total time of 8 hours, but when he switched to a Huayuan HDR-300, he calculated his cut-through time for 2-inch plate was 0.9 seconds (vs. 1.8 seconds on the competitor’s machine). That cut his total job time to 4.5 hours, and he won the bid because he undercut the competition by 10%. That’s not hype — that’s the difference a consistent, well-calibrated plasma cutter makes on thick metal.
Now, if you’re in the market for a Huayuan plasma cutting machine, here’s what I recommend you ask yourself to narrow down your needs: what’s the maximum thickness of metal you’ll be cutting most often? What metals (mild steel, stainless, aluminum) are you working with? How many pierces do you run per day? If you’re mostly cutting 1-2 inch mild steel, a 200-amp Huayuan system will give you cut-through times that are 30-40% faster than most mid-range brands. If you’re doing 3-4 inch thick metal, step up to a 300 or 400-amp system, and you’ll get the same consistent cut-through time that saves you time and money.
I talk to fabricators every day who have spent thousands on machines that don’t deliver on thick metal, and the number one mistake I see is not factoring in cut-through time into their initial budget. A $10,000 plasma cutter might sound cheap, but if its cut-through time is double what a Huayuan system’s is, you’ll be paying $5,000 in lost productivity every year. Huayuan builds our systems with that in mind — we test every machine for 24 hours straight on thick metal before it leaves our factory, so you don’t have to guess if it’ll hold up on your shop floor.

If you’re currently dealing with slow cut-through times on thick metal, or if you’re ready to upgrade your plasma cutting machine to save time on your jobs, I’m here to help. Whether you’re a small custom metal shop or a large fabrication facility, I can walk you through the specific cut-through times for your exact metal thickness and type, and help you pick the right Huayuan system that fits your needs and budget. Don’t let cut-through time slow you down on your next big job — reach out today to talk through your requirements, and we’ll get you set up with a machine that performs when you need it most.
Handheld Laser Cleaning And Rust Removal Machine References
- Huayuan Plasma Technology. (2023). Specification Manual for HDR Series Precision Plasma Cutting Systems.
- Kochan, D. (2022). Plasma Cutting Fundamentals for Industrial Fabrication. Industrial Press.
- American Welding Society. (2021). Guide to Thermal Cutting Processes for Thick Metal Applications.
Hebei Juliang Technology Co., Ltd.
Hebei Juliang Technology Co., Ltd. is one of the most professional plasma cutting machine for huayuan manufacturers and suppliers in China, featured by quality products and good service. Please rest assured to buy CE approved plasma cutting machine for huayuan from our factory. Welcome to contact us for customized service and discount information.
Address: Building 1, Juluang Industrial Park, Gaocheng District, Shijiazhuang City, Hebei Province, China
E-mail: sales@jlwmb.com
WebSite: https://www.julasers.com/
