Hey everyone, thanks for swinging by my corner of the web. I’m Jake, and I’ve been selling brick machines for over 12 years now—seen a lot of production lines come and go, and even more owners scratching their heads over why their output’s stuck, or their bricks are inconsistent, or they’re burning through cash on wasted materials. If you’re here because you’re trying to get more out of your brick machine line, not just keep it running, you’re in the right spot. No stuffy corporate jargon, just real stuff I’ve picked up on job sites and from working with hundreds of production teams. Brick Machine
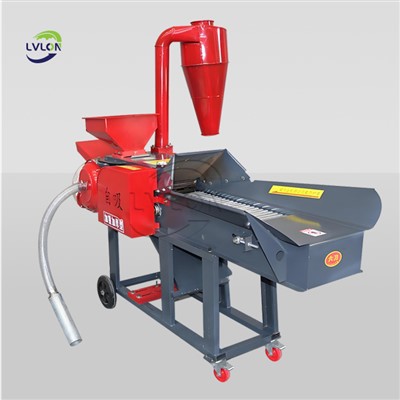
First off, let’s get one thing straight: optimizing a brick line isn’t just buying a “better machine.” It’s tying every part of the process together, from mixing the raw clay to stacking finished bricks. I’ve seen a shop with a 5-year-old machine crank out 15% more bricks a day than a place that dropped $20k on a fancy new model—because they didn’t fix the gaps between each step. Let’s break this down into the stuff that actually moves the needle, no fluff.
Let’s start with the raw material prep, because this is where 70% of avoidable waste comes from. You can have the fanciest extruder or mold, but if your clay’s got rocks, uneven moisture, or wrong particle size, you’re going to have defects, downtime, and half the bricks breaking before they even hit the drying rack. A lot of guys skip the simple checks here. I always tell clients: test your clay every morning, not once a week. Here’s what to look for: moisture content between 12-15%. Too dry, and the extruder struggles to push it through, wears out the die faster. Too wet, and the drying stage takes twice as long, leading to bottlenecks. How to test it quick? Grab a handful, squeeze it tight in your fist. If it holds a shape but doesn’t leak water, you’re golden. If it leaks, add some dry sand or crushed old brick dust (recycling your own rejects is a trick I swear by). If it crumbles when you open your hand, spritz a little water from a spray bottle—no need to dump a whole bucket.
Then, screen your raw material. A lot of people skimp on the screener, just dumping clay straight into the hopper. But if you’ve got chunks bigger than, say, 5mm, those will either jam the extruder or cause cracks in the bricks. I’ve worked with a team that added a simple vibrating screener for $800, and their reject rate dropped by 11% in a month. Worth every penny. Pro tip: save all your broken bricks and offcuts, crush them into a fine powder, and add them back to the mix. It cuts down on clay use and actually improves the strength of the finished bricks. Win-win.
Next up, the machine operation itself. This is where even small tweaks add up big. First, get your operator trained right—don’t just hire a guy who can turn a key. A good operator knows the machine’s rhythm. For example, on a hydraulic brick machine, if you run the press at full pressure for just a second longer, you get bricks that are denser, so they don’t break in the kiln. But if you hold it too long, you waste power and slow down the cycle. I do 1-hour training sessions for all my clients when they buy a machine, and half the time we adjust their cycle times by 2-3 seconds per press. Multiply that by 1,000 presses a day, and that’s an extra 50 bricks an hour—no extra work, just adjusting the rhythm.
Also, routine maintenance isn’t just “fix it when it breaks”—it’s scheduled, small tasks that keep downtime from happening. I see guys forgetting to clean the die every shift, or lubricate the chain on the conveyor, and then the machine seizes up at 2 a.m. on a Friday, costing them a whole day’s production. Here’s a maintenance checklist I give every client: wipe the die clean with a dry rag every 8 hours, check the oil levels before each shift, tighten loose bolts on the machine frame once a week, and replace the die seals every 3 months (even if they look fine). A $20 seal replacement beats a $2,000 repair bill any day. Oh, and keep a spare set of dies on hand—don’t wait for one to break before you order another. I know guys who had to shut down for 3 days waiting for a die to ship, just because they skipped having a spare.
Now, the drying stage—this is the biggest bottleneck in most brick lines, trust me. If your bricks are wet when they go into the kiln, they’ll crack, warp, or even explode. If they’re too dry before firing, you lose strength. The sweet spot is drying them to 1-2% moisture content. A lot of shops just use open-air drying, which takes 2-3 days, and depends on the weather. If it rains, you’re toast. So, what’s the fix? A simple enclosed drying chamber, even a temporary one made with tarps and fans, cuts drying time to 18-24 hours, no matter the weather. I worked with a place that was using open drying and had 30% of their bricks ruined in monsoon season; they added a 10×12 drying room with 4 exhaust fans for $1,200, and their reject rate dropped to 5%. Game changer.
Another trick here: stack your bricks correctly in the drying racks. If you stack them too tight, air can’t circulate, so some stay wet longer. If you stack them too loose, you waste space. The standard is to leave a 1-inch gap between each brick layer, and 2 inches between the sides of the stack and the wall of the drying room. That way, every brick dries evenly, no hot spots. I’ve seen guys cram as many as possible, and end up with half the batch having uneven moisture. Don’t do that.
Then the kiln stage—this is where you’re turning green bricks into finished product, and it’s where energy costs eat into profits more than any other part. First, check your kiln’s temperature uniformity. A lot of small kilns have hot spots on one side and cold spots on the other, leading to some bricks being under-fired (weak) and some over-fired (costing extra energy). How to fix that? Add a few extra thermocouples (temperature sensors) if you don’t have them, and adjust the airflow in the kiln. If a side is too cold, open the vent there; too hot, close it. I had a client who was using 15% more gas than needed because his kiln vents were all set the same; we adjusted them, and his gas bill dropped by $180 a month. That’s $2,160 a year, just from tweaking vents.
Also, use the heat from the kiln to pre-dry bricks. A lot of guys heat their kiln, and then just vent all the hot air out. You can run a duct from the kiln’s exhaust to your drying room—free heat! That cuts the energy needed for drying by 40%, and also means you’re using less gas to heat the kiln. I know this sounds too simple, but it’s one of the most underused tricks in the industry. I’ve installed that ducting for dozens of clients, and it’s paid for itself in 2-3 months.
Now, let’s talk about line integration—this is the part that most people miss. Your brick machine is only as good as the step before and after it. If your mixer can only feed 50 bricks an hour, and your press can do 60, you’re wasting 10 bricks an hour, and your mixer is going to wear out faster. The same goes for stacking: if your conveyor can’t move bricks fast enough to the drying racks, the press is sitting idle. The fix here is to match the capacity of every machine. For example, if you have a 500 bricks per hour press, get a mixer that can mix enough clay for 500 bricks an hour, a conveyor that can move 500 bricks an hour, and a drying rack system that can hold 500 bricks. I’ve seen guys buy a big press first, then stretch and skimp on the other equipment, and end up with only 70% of the press’s actual output. That’s like buying a sports car and only driving it 20 mph—wasting all that potential.
Also, automate where you can, but don’t go overboard. Full automation is great for big shops, but if you’re a small to medium operation, a semi-automated setup is cheaper and just as effective. For example, instead of stacking bricks by hand, get a simple hydraulic stacker that costs $1,500, and it will move 500 bricks an hour without tiring out a worker. No more human error from stacking too tight or too loose, and you save labor time. I worked with a small shop that was doing all stacking by hand; they added the stacker, and their daily output jumped from 3,000 bricks to 4,200—no extra workers, just that machine.
Wait, let’s talk about data—because even small shops can track stuff now, no fancy software needed. Keep a log every day: how many bricks you made, how many were rejects, what the moisture was, how much gas you used. After a month, you’ll see patterns. For example, you might notice that every time the moisture is under 13%, your reject rate goes up. Or that when the kiln is over 900 degrees, you use 10% more gas. That data lets you fix small problems before they turn into big ones. I used to give clients a free simple log sheet when they bought a machine, and almost all of them said it helped them cut their costs by 10-15% within two months.
Now, let’s hit the common mistakes I see all the time. First, ignoring old parts because they “still work.” That $50 worn-out part might cause a breakdown that costs you $500 in lost production. Second, not training operators—every time you hire a new operator, you’re risking downtime because they don’t know the machine’s nuances. Third, skipping recycle. Like I said earlier, all your broken bricks and offcuts can be crushed and reused. I know a guy who was throwing away 200 bricks a day, just because they were chipped; he started crushing them, and saved $120 a month on clay. That’s free money.
Another mistake: not testing new materials. If you switch to a different clay source, don’t just jump in—do a small test run first. Test the moisture, test the extrusion, test the drying. I’ve had clients switch to a cheaper clay, not test it, and end up with 40% of their bricks cracked in the kiln. It’s not worth saving $50 on clay if you lose $500 in rejects.
Now, let’s wrap this up with what actually matters. Optimizing your brick line isn’t about the newest, biggest machine—it’s about making every part work in sync, wasting as little as possible, and taking small steps to cut costs and boost output. I’ve seen shops that were on the brink of closing turn profitable just by doing these things, no huge investment.
If you’re tired of dealing with bottlenecks, high reject rates, or sky-high energy bills on your brick line, I can help. I’ve worked with hundreds of brick production teams, from small 100-brick-a-day operations to commercial sites doing 10,000 bricks a day, and I can help you figure out what tweaks will work for your specific setup. Whether you need advice on maintenance, material prep, kiln adjustments, or even picking the right machine to upgrade, just reach out to chat. No sales pitch, no pressure, just real advice from someone who’s been in this for years.
Before I go, a quick note for anyone who wants to dive deeper into the science here—those looking for more technical details on moisture content, extrusion pressure, or kiln heat transfer can check out these resources on brick production optimization:
- Handbook of Clay Brick Technology, published by the International Brick and Block Association
- Journal of Manufacturing Processes (2021) study on reducing reject rates in small-scale brick production
- Practical Guide to Brick Manufacturing, from the United Nations Industrial Development Organization (UNIDO)
Crusher Machine That’s it for today. Hope this saves you some time and money on your brick line. Catch you next time.
Henan Lvlon Industrial Co., Ltd.
Address: Unit 5, 5th Floor, Building 11, No. 18 Dongfeng Road, Jinshui District, Zhengzhou City, Henan Province.
E-mail: lvlonxu@gmail.com
WebSite: https://www.lvlonmachinery.com/
